Project Case
Home >> Project Case >> Reliable Valve Solutions for Advanced Chemical Processing
Project Name: Fujian Baihong Chemical Integrated Chemical Project
Industry: Chemical Processing
Project Scope: 150,000 TPA n-Butane to Maleic Anhydride Unit, 200,000 TPA CO₂ Recovery Unit, and 200,000 TPA Ethylene Carbonate Unit
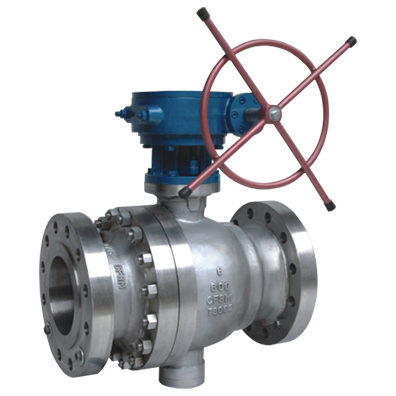
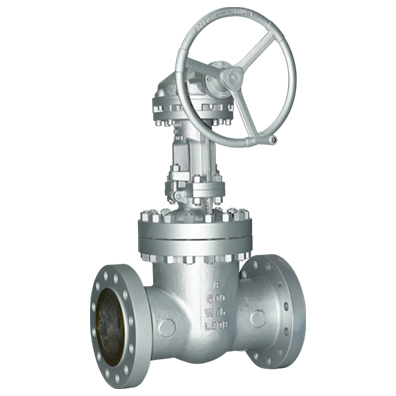
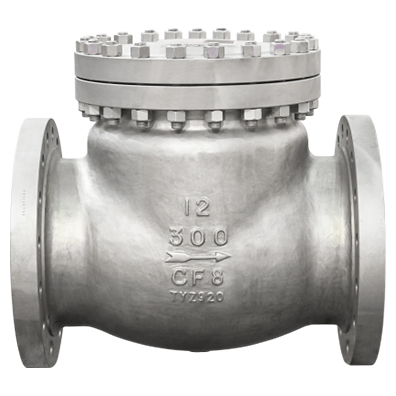
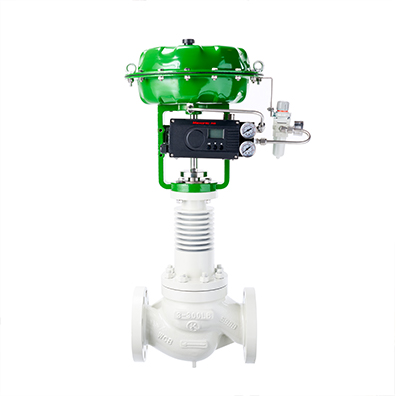
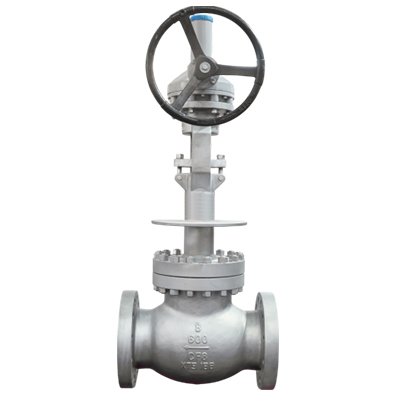
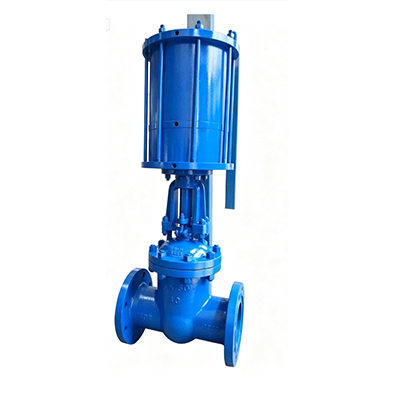
Valve Solutions: Manual Ball Valves, Gate Valves, Check Valves, High-Temperature Control Valves, Globe Valves, Pneumatic Gate Valves
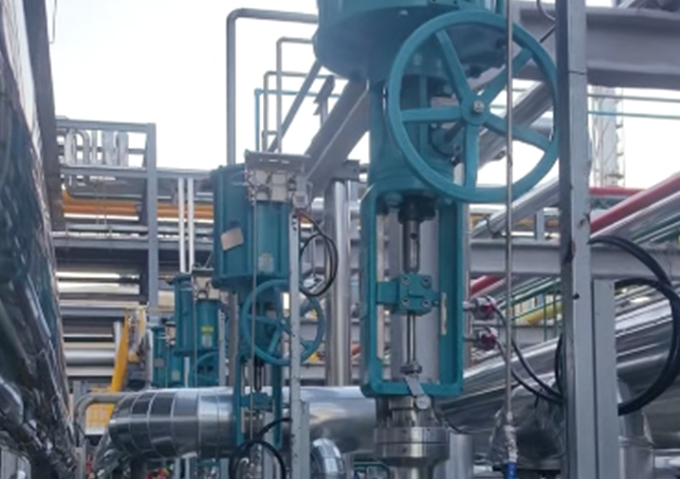
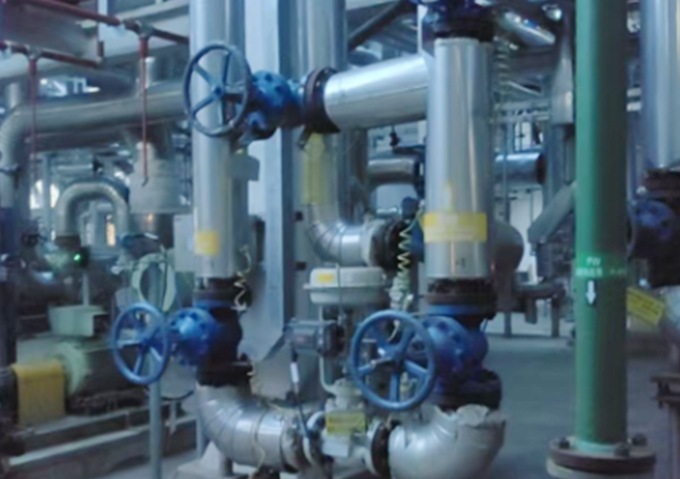
Fujian Baihong Chemical invested in multiple advanced chemical production units, including a 150,000 TPA n-butane to maleic anhydride plant, a 200,000 TPA CO₂ recovery facility, and a 200,000 TPA ethylene carbonate production unit. The project requires reliable valve solutions capable of operating under high temperatures, corrosive media, and continuous-duty conditions while ensuring safe and efficient process control.
High-temperature process media requiring reliable sealing performance
Corrosive chemical environments demanding excellent material resistance
Continuous operation with strict requirements for long service life and operational stability
Precise process control in critical production units
Reliable isolation and backflow prevention to ensure plant safety and efficiency
What We Provided
We supplied a complete range of industrial valve solutions, including:
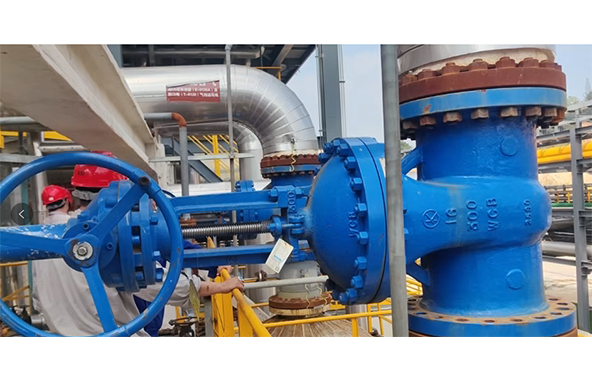
1Manual Ball Valves
2Gate Valves
3Check Valves
4High-Temperature Control Valves
5Gate Valve
6Pneumatic Gate Valves
Each valve was engineered and manufactured according to the project's operating conditions, ensuring reliable sealing, stable operation, and long-term durability.
Products Supplied
Project Results
· Multi-Unit Valve Application: Valve solutions were successfully deployed across the n-Butane to Maleic Anhydride, CO₂ Recovery, and Ethylene Carbonate production units.
· Severe-Service Adaptability: High-temperature and corrosion-resistant valve solutions provided dependable performance for demanding chemical process conditions.
· Automated Operation: Pneumatic gate valves and control valves supported efficient operation and centralized process management.
· Process Safety Support: Reliable isolation and check valve performance helped enhance system safety and prevent unintended backflow.
Hangzhou Kaiwei Valve Group Co, Ltd, established in 2015, is a cutting-edgeindustrial enterprise that specializes in the R&D, design, casting, production,and sales of fluid control products and services
Contact Us